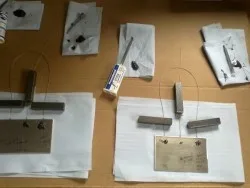
Client: Creative design company
Adhesive: 2C Epoxy
Substrates: Test: PE - Final application: Aluminium
Year: 2013
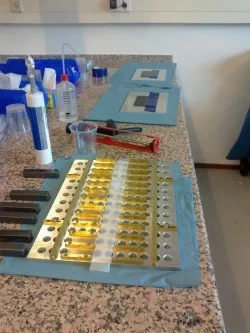
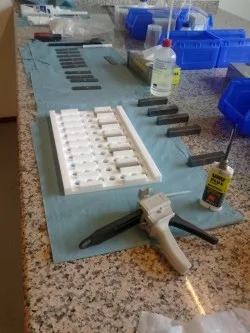
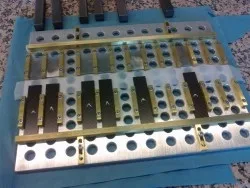
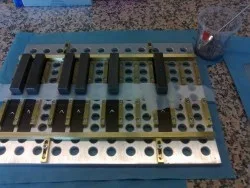
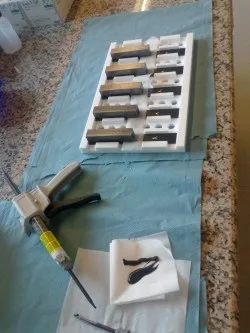
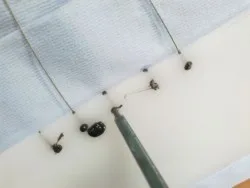
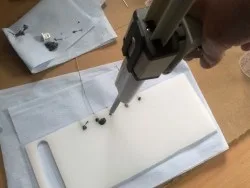
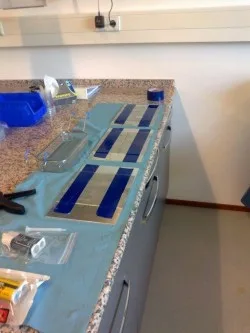
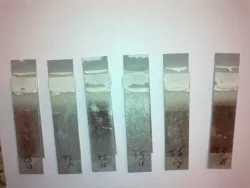
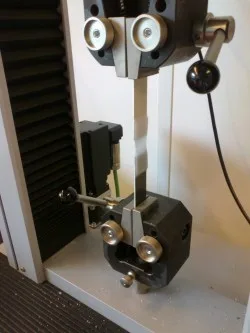
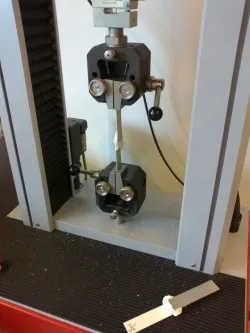
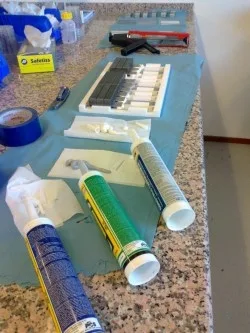
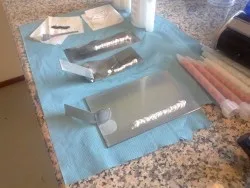
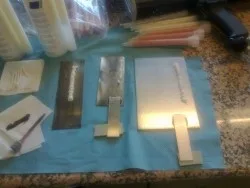
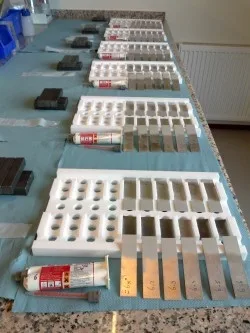
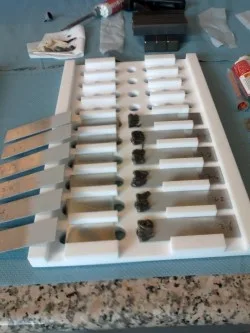
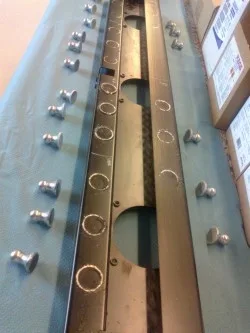
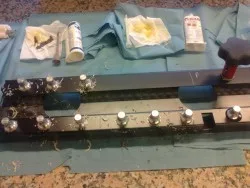
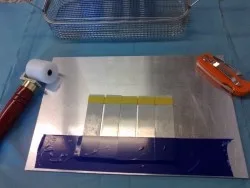
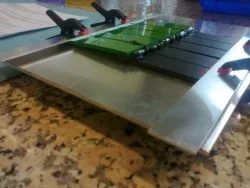
Results: By adding a tiny filling hole at the side, it became possible to clean the complete surface area and to fill the hole with adhesive. The used PE material was slightly transparant so it was easy to see the dark color adhesive filling the complete hole.
Client: Manufacturer of building components and a repair company in the construction sector
Adhesive: MS Polymer, Silicones, 1C PU and MMA
Substrates: Coated aluminum and plastic
Year: 2014
Results: Binder MKF 115 E3.1
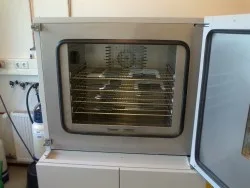
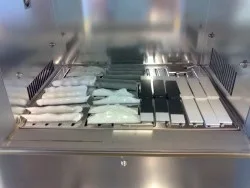
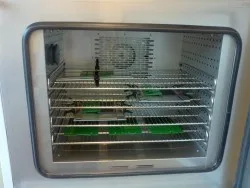
During weeks alternating climate (ISO 9142 cycle D3), with a day-cycle of:
=> 15 hour at 70 °C and 90% RH
=> 1 hour transition
=> 2 hour at -20 °C
=> 1 hour transition
=> 4 hour at 70 °C and 50% RH
=> 1 hour transition
Results are confidential
Client: Manufacturer of construction elements and construction repair company
Adhesive: MS Polymeer, Siliconen, 1C PU and MMA
Substrates: Coated aluminium and plastic
Year: 2014
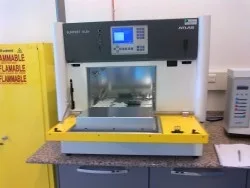
Results: Xenon UV with waterspray: Suntest XLS+ with Atlas Sunspray
During 4 weeks Xenon-UV with waterspray (ISO 4892-2:2013, Table B.1 - Method A -
Cycle no. B1). Artificial aging using a Xenon-lightsource (300 nm - 400 nm) with daylight filter and waterspray.
Client: Supplier of tape-products
Adhesive: Doublesided and transfertape
Substrates: Aluminium 1,5 [mm]/aluminium 0,5 [mm]
Year: 2014
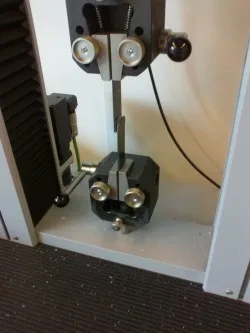
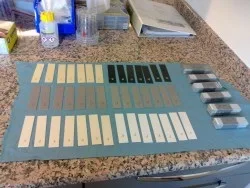
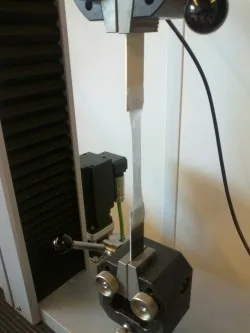
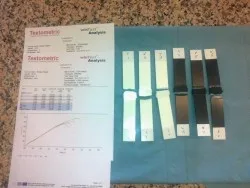
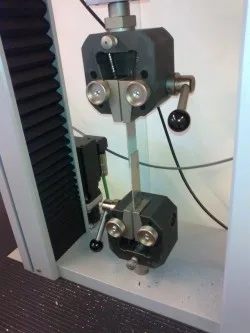
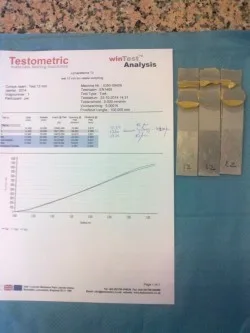
Results: Several rollerpeeltests performed (EN 1464)
Results are confidential
Client: Industrial supplie
Adhesive: Transfertape
Substrates: Rubber (SBR)
Year: 2014
Results: Using AD Plasma as surfacepretreatment, the adhesion on the surface of the substrate became sufficient. More important: the proces became much more reproducible and predictable.
Client: Construction company
Adhesive: Several PSA types
Substrates: PE
Year: 2014
Results: Quick scan using AD Plasma or primer-treatment and several PSA types
Result: Tape-product selected with which cleaning with IPA is sufficient
Client: Designcompany
Adhesive: 2C Epoxy
Substrates: Concrete/plastic
Year: 2014
Results: Adhesive bonding of plasticparts in partly sawn out floortiles
Client: Manufacturer of high-tech components
Adhesive: 2C Epoxy
Substrates: Aluminium/aluminium for testprocedure
Year: 2014
Results: Testresults comply with data from Technical Data Sheets.
Reconsider applicationmethod to solve quality problems on bonded joints.
Client: Expertcenter in coatings
Adhesive: MMA
Substrates: Aluminium/(coated)aluminium
Year: 2014
Results: Yet to be discussed with the equipment supplier.
Client: Contractor in construction
Adhesive: PSA (extremely flexible double-sided tape)
Substrates: Coated aluminium
Year: 2014
Results: Surprisingly good adhesion and deformation behavior
Client: Contractor in buildng and construction
Adhesive: MS Polymeer, Silicon, PSA
Substrates: Coated aluminium
Year: 2014
Results: Quick scan helped to select three out of seven types of adhesive to continue with accelerated aging tests.
Client: Supplier to the shipbuilding industry and metalcontracting company
Adhesive: 2C Epoxy and MS Polymer
Substrates: Titanium, plastic, lead, glvanized steel
Year: 2013 & 2014
Results: Adhesive products and surfacetreatment-methods selected, meeting requirements
Client: Supplier to railvehicle manufacturers and aircraft industry
Adhesive: Transfertape
Substrates: Aluminium/cork
Year: 2014
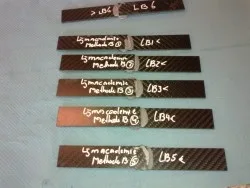
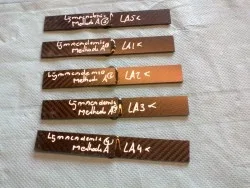
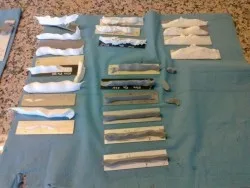
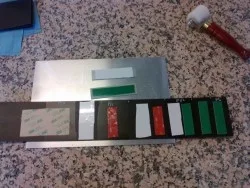
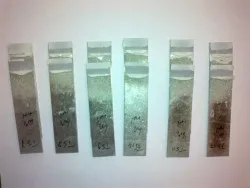
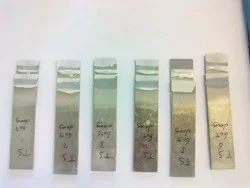
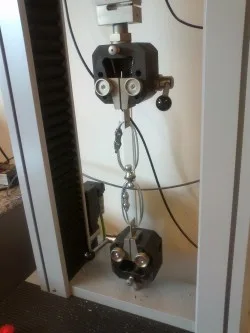
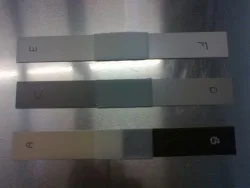
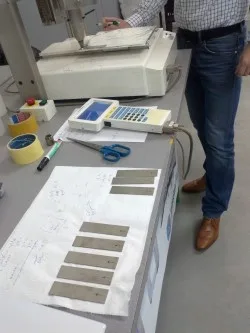
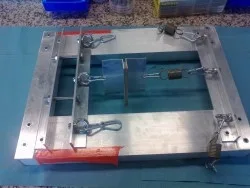
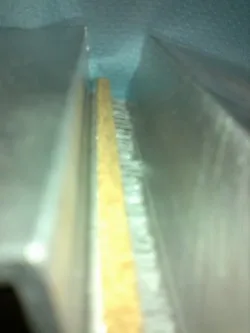
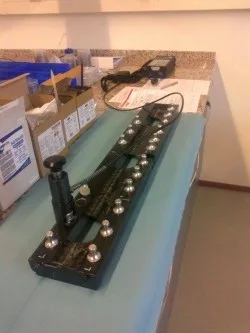
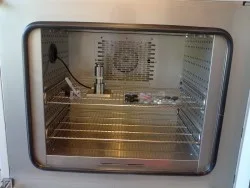
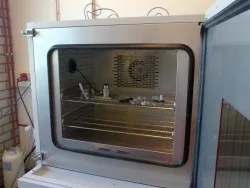
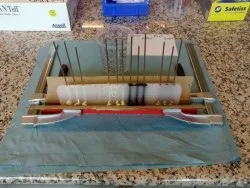
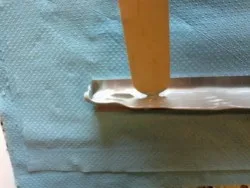
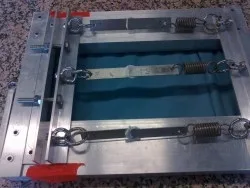
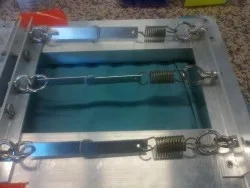
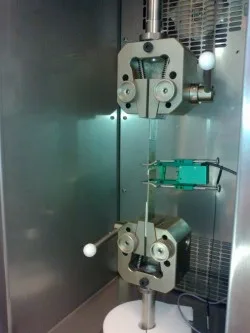
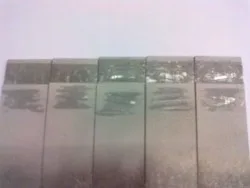
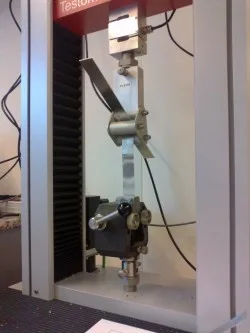
Results: Special frame is used to tension adhesively bonded joints. Tested both on roomtemperature an in the oven at 80 °C. Clear shift in adhesive failure patern from cohesive (as shown in picture below) into adhesive as soon as testtemperature raises.
Client: Manufacturer of sandwich panels fr the transportation sector
Adhesive: 2C PU
Substrates: Polyester and foam
Year: 2012, 2013
Results: The adhesive bond failed mainly due to moisture damaging the adhesive
Client: Manufacturer of hightech metalsheet products
Adhesive: MMA
Substrates: Stainless and KTL-treated carbon steel in applicatie, aluminium to perform tests
Year: 2014
Results: Results are confidential
Client: Manufacturer in the metalworking industry
Adhesive: n.a
Substrates: KTL-treated steel
Year: 2014
Results: Tests performed with pens, inks and PGX+ goniometer
Results are confidential
Client: Manufacturer in the metalworking industry
Adhesive: MMA and 2C Epoxy
Substrates: KTL-treated steel
Year: 2014
Results: Quick scan by testing several adhesive products by means of dolly-test.
Results are confidential
Client: OEM in the transportsector
Adhesive: MS Polymer
Substrates: Plastic, aluminium
Year: 2013
Results: Observation of the productionprocesses lead to several suggestions for improvement. Changing the cleaning and primer-application processes improved the reproducibility and predictability. Additional direct costsavings on consumables by itself already made up for the costs of the observationround within half a year.
Client: Supplier shipbuildingindustry, hightech metalsheetproducts and designcompany
Adhesive: 2C Epoxy, MMA
Substrates: Titanium, platic, KTL treated steel, Stainless steel, aluminium
Year: 2013, 2014
Results: Using simple testmethods, a first selection of suitable adhesive products can be made. Next step is to test these selected adhesives in bonded joints by means of accelerated aging.
Client: Repaircompany in building and construction
Adhesive: MMA
Substrates: Plastic/plastic
Year: 2014
Results: Using two types of accelerated aging equipment (alternating climate and Xenon-UV-moisture) adhesive bonded joints were tested. The results confirmed the repairmethod to be suitable for an outdoor application.
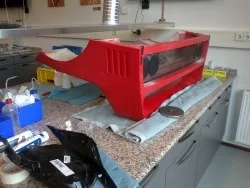
Client: Studentproject Delft University of Technology, Ferrari F40 replica, goalkeeper helmet, participant's shoe
Adhesive: MMA, diffusionboning and cyanoacrylaat
Substrates: Plastic, aluminium, foam, fabrics, rubber
Year: 2014
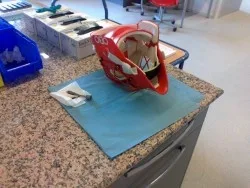
Results: Knowledgetransfer and actual adhesively bonded joints
Client: Supplier and expert in labinstruments
Adhesive: Not disclosed
Substrates: n.a
Year: 2014
Results: Confidential
Client: Supplier of MS Polymer
Adhesive: MS Polymers of four different suppliers
Substrates: Metals, plastics, glas, wood
Year: 2014
Results: Lapshear-/adhesiontests on seven different substrates. Creeptest, skinformingtest, curingtest performed at client approved methods.
Measurementresults: confidential
Client: High-tech company
Adhesive: 2C Epoxy with high level silver content
Substrates: Aluminium
Year: 2014
Results: Reasonable results of the Young-modul at temperaturelevels 20 °C till 140 °C. Additional (optical) surface analyses.
Client: Supplier of tape products
Adhesive: Doudle sided tape
Substrates: Aluminium
Year: 2014
Results: Lapshear- and rollerpeeltest results
Client: Plastic company
Adhesive: MS Polymer and 1C PU
Substrates: Plastic/plastic
Year: 2014
Results: Results are not published
Client: High tech producer
Adhesive: 1C Epoxy, silicone masking tape
Substrates: Aluminium
Year: 2014
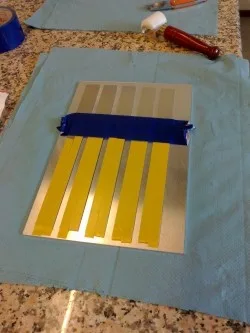
Results: It is possible to use masking tape in improving a more accurate adhesive bonded area. In this case the increased adhesive layer thickness caused more inaccuracy than the improvement by more accurate adhesive bonded area's.
Client: Manufacturers of parts for railvehicles
Adhesive: 2C Polyurethane
Substrates: Alumium
Year: 2014
Results: Destructive testing on series of processcontrol samples showed a slow change in strength of the adhesive application in the factory.
Client: None (internal project)
Adhesive: Two types MMA, two types 2C Epoxy (80 °C) and one type 1C Epoxy (180 °C)
Substrates: Aluminium-aluminium - Corund grind / MEK Ultrasoon cleaning
Year: 2014
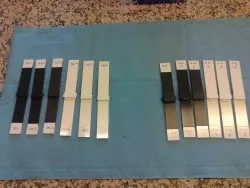
Results: Aging during 0, 14 and 28 days with cycles 5 hour +/+80 °C >90% RH and 5 hour -/-40 °CSpecial:
Results will become available in December. Report will be for sale for Euro 73,50 excl. VAT and transportcosts
If you are interested, please send a message to info@makiba.eu